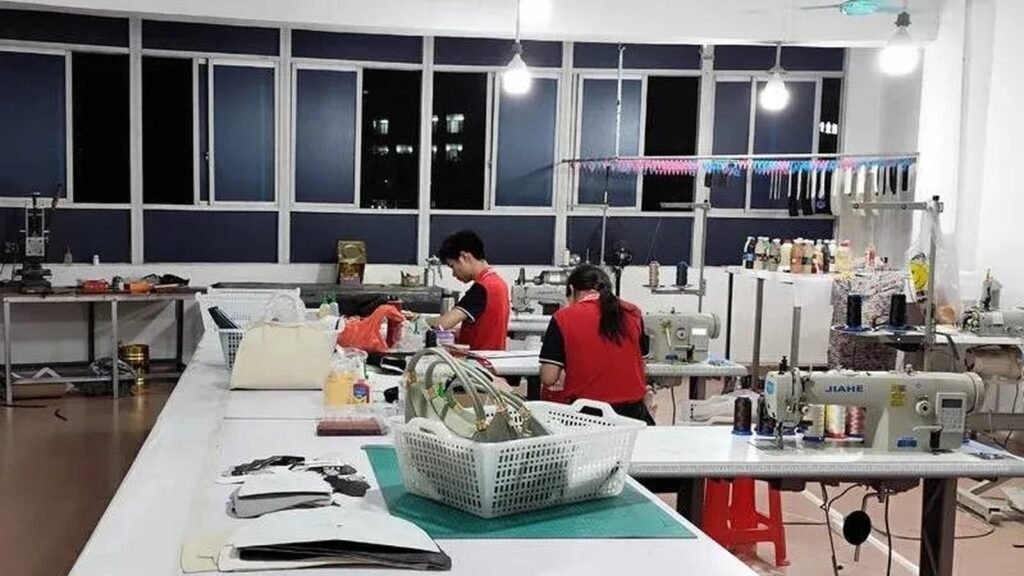

China makes the majority of the world’s bags—backpacks, handbags, luggage, wallets, and laptop cases. Unit prices are a fraction of Western retail, and private-label customization is straightforward. But bags fail in predictable ways: broken zippers, torn seams, weak handles, and suitcase wheels that crack after two trips. This guide covers materials, hardware, QC checkpoints, MOQs, and the manufacturing clusters to target.
1. Categories and Materials
- Backpacks and laptop bags. Usually polyester or nylon (420D, 600D, 900D denier). Higher denier = tougher. PU leather trim is common for premium looks.
- Handbags and wallets. PU leather dominates the mid-market; genuine leather is used for high-end goods. Watch for “genuine leather” claims that are actually split leather or bonded leather.
- Rolling luggage. PC (polycarbonate) shells are lightweight and impact-resistant; ABS is cheaper but heavier. Look for aluminum trolley systems and quiet spinner wheels.
- Travel accessories. Cosmetic bags, duffels, packing cubes—usually polyester with custom printing.
2. Hardware: Zippers and Buckles That Make or Break the Bag
Most bag complaints trace back to hardware. Specify on your PO:
- Zippers. YKK is the premium standard; SBS and YCC are acceptable budget alternatives. Avoid unnamed zippers.
- Sliders and pulls. Metal sliders outlast plastic; pulls should be riveted, not glued.
- Buckles and snaps. Test for 500+ open/close cycles; zinc alloy is better than iron.
- Luggage wheels. Double spinner wheels with sealed bearings roll smoothly; cheap wheels crack within months.
3. QC: The Defects That Actually Happen
Inspect these points before shipment:
- Stitching. Even stitch density, no skipped stitches, no loose threads. Stress points (handles, straps) should have reinforced bartacks.
- Zipper function. Run every zipper 10 times; it should not snag or separate.
- Weight test. Backpacks and luggage should hold 2–3 times their rated load without strap failure.
- Symmetry and alignment. Pockets, straps, and logos must be centered; crooked stitching is the #1 visual defect.
- Material match. Confirm the spec’s denier and leather grade against the sample—factories quietly downgrade fabric.
4. MOQ and Sampling
Typical MOQs from Chinese bag factories:
- Custom backpacks with your logo: 300–500 pcs
- Handbags/wallets: 200–500 pcs
- Rolling luggage: 300–500 pcs (mold cost may apply for custom shapes)
- Printed polyester accessories: 500–1,000 pcs
Sample fees range USD 50–200 per style, refundable at bulk order. Approve the physical sample in writing before mass production—this is the single most effective step to prevent sample-to-bulk mismatch.
5. Manufacturing Clusters: Where to Source What
- Guangzhou Huadu (Guangdong). Handbags, ladies’ bags, leather goods. The densest leather-bag cluster in China.
- Pinghu (Zhejiang). Backpacks, school bags, laptop bags. Strong for mid-market everyday bags.
- Baigou (Hebei). Budget luggage, wallets, briefcases. Best for price-sensitive mass-market goods.
- Quanzhou (Fujian). Backpacks and outdoor bags.
Private-label customization—your logo, colors, interior lining, and packaging—is standard across all clusters. Communicate tech packs (dimensioned drawings, material specs, Pantone colors) rather than relying on verbal descriptions.
6. Pricing: What Makes a Bag Expensive or Cheap
The same backpack design can range from USD 3 to USD 30 FOB. The drivers are: fabric denier and quality, hardware brand (YKK vs no-name), lining material, zipper and buckle grade, stitching precision, and packaging. A USD 8 backpack from Baigou with no-name zippers will look fine in photos but will fail within months; a USD 18 bag from Pinghu with YKK zippers and reinforced straps will last years. Always ask the factory to list the brand of every hardware component—that single line item explains most of the price gap.
For luggage, the big cost variables are shell material (PC vs ABS), trolley system (aluminum vs steel), wheel quality, and interior organizer design. Specify each on your tech pack, and ask for a sample before committing to a 500-piece order.
7. Common Sourcing Mistakes to Avoid
The most expensive bag-sourcing errors are: choosing a supplier based only on price without checking hardware brands; approving a sample but not a production sample; skipping the weight test on straps; and not specifying fabric denier on the PO. Another common mistake is ordering custom luggage shapes without accounting for mold fees—these can run USD 3,000–10,000 and are non-refundable. Start with catalog shapes, prove the model, then invest in custom tooling once sales data justifies it. For most new bag brands, the winning formula is: pick a proven catalog style, upgrade hardware to YKK, specify slightly heavier fabric, and private-label your logo and packaging. This beats trying to design a fully custom bag on the first order—the tooling cost and risk are far higher, and the market rarely rewards it. Once a style sells well, you can iterate on it with custom colors, upgraded lining, and private-label packaging without re-engineering the bag itself.